P20+S Plastic Mold Steel
1.2312
- EN1.2312
- EN40CrMnMoS8-6
- AISIP20+S
Plastic mold steel delivered pre-hardened (28–32 HRC). Because of its sulphur content 1.2312 is not suitable for texturing; where uniform core hardness and better polish are required, 1.2738 should be preferred. Offers excellent machinability.
01Material Properties
- Very easy to machine despite being pre-hardened
- Easy deep-hole drilling
- Can be machined at high speed and feed
- Uniform hardness distribution across sections up to 300 mm
- Use 1.2738 where polishing, texturing or welding is required
- Recommended working hardness is the delivery hardness
- Suitable for nitriding
02Applications
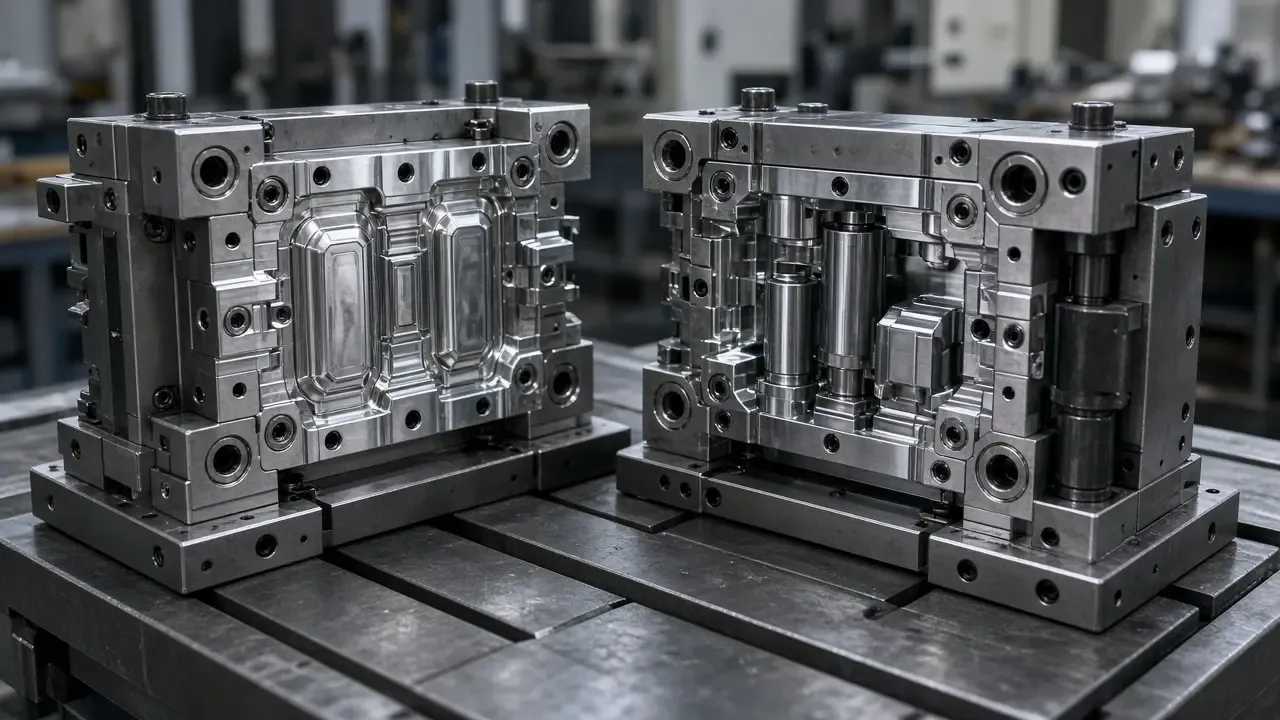
- Cores of non-visual plastic injection molds
- Preferred for the core side of injection molds
- Plastic injection mold holders
- Metal injection mold holders
- Machine parts, wear plates
03Delivery Condition
- Pre-hardened, 280–320 HB
04Heat Treatment
Typical values
- Delivery condition
- Pre-hardened 280–325 HB
- Stress relieving
- 550–600 °C after rough machining; furnace cooling
- Re-hardening
- 840–870 °C, oil → ≈ 50–52 HRC
- Tempering (after re-hardening)
- 500–600 °C → 30–40 HRC
- Nitriding
- Limited effectiveness due to sulphur
Heat treatment cycle (schematic)
Tempering diagram (approximate)
Values are approximate and for information only; they vary with section size, heat and furnace conditions. Binding values are determined from the manufacturer’s data under laboratory conditions.
Have a material requirement?
Send us your specification, drawing or RFQ. Our team will review the requirement and identify a suitable supply option.