1.2162 Case-Hardening Mold Steel
1.2162
- EN1.2162
- EN21MnCr5
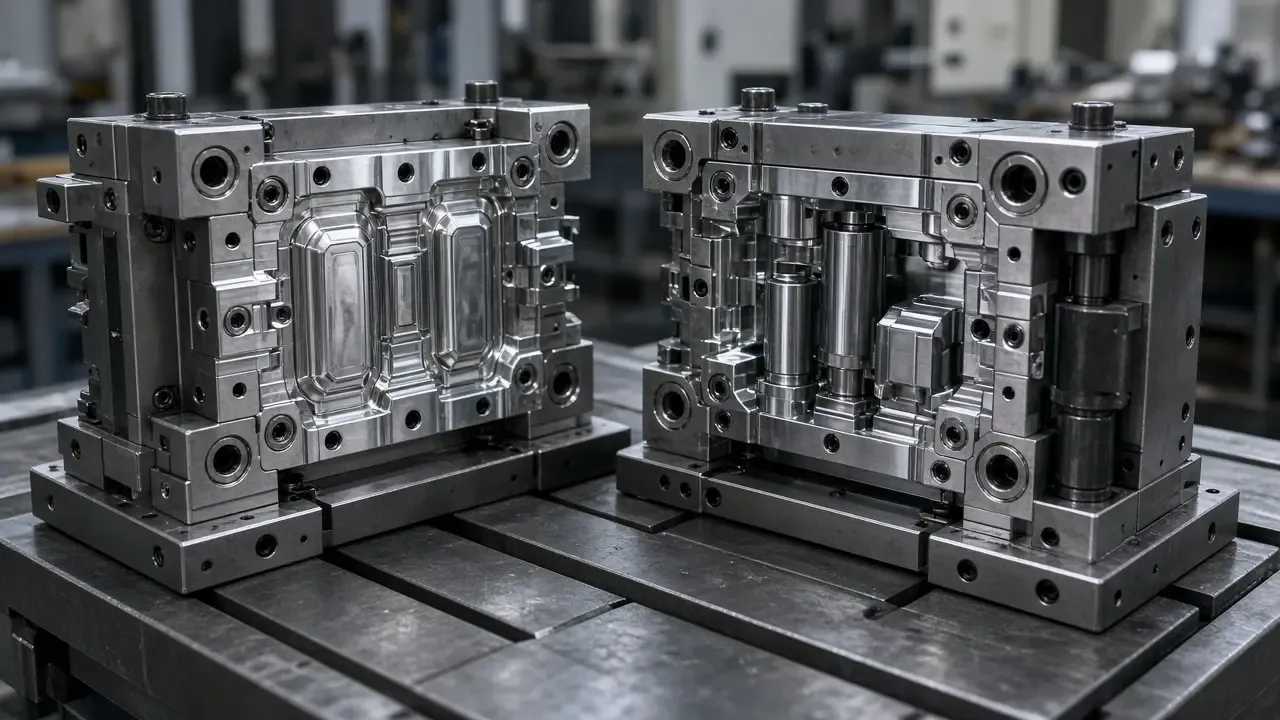
Case-hardening mold steel. Easy to machine and hob in the soft condition; after carburising it provides a hard, wear-resistant surface with a tough core.
01Material Properties
- Easy machining and hobbing in the soft condition
- Surface hardness 58–62 HRC after carburising
- Tough core, impact resistance
- Good polishability
- Suitable for small and medium sections
02Applications
- Small and medium plastic injection molds
- Mold cavities produced by hobbing
- Cores, pins and slides
- Gears and machine components
03Delivery Condition
- Max. 217 HB, soft annealed.
04Heat Treatment
Typical values
- Soft annealing
- 650–700 °C; max. 217 HB
- Carburising
- 880–980 °C; 0.5–1.5 mm case depth
- Hardening
- 820–850 °C, oil (core); 780–820 °C (case)
- Tempering
- 150–200 °C, 1–2 h
- Surface hardness
- 58–62 HRC
- Core
- ≈ 30–40 HRC, tough
Heat treatment cycle (schematic)
Tempering diagram (approximate)
Values are approximate and for information only; they vary with section size, heat and furnace conditions. Binding values are determined from the manufacturer’s data under laboratory conditions.
Have a material requirement?
Send us your specification, drawing or RFQ. Our team will review the requirement and identify a suitable supply option.