D2 Tool Steel
1.2379
- EN1.2379
- ENX153CrMoV12
- AISID2
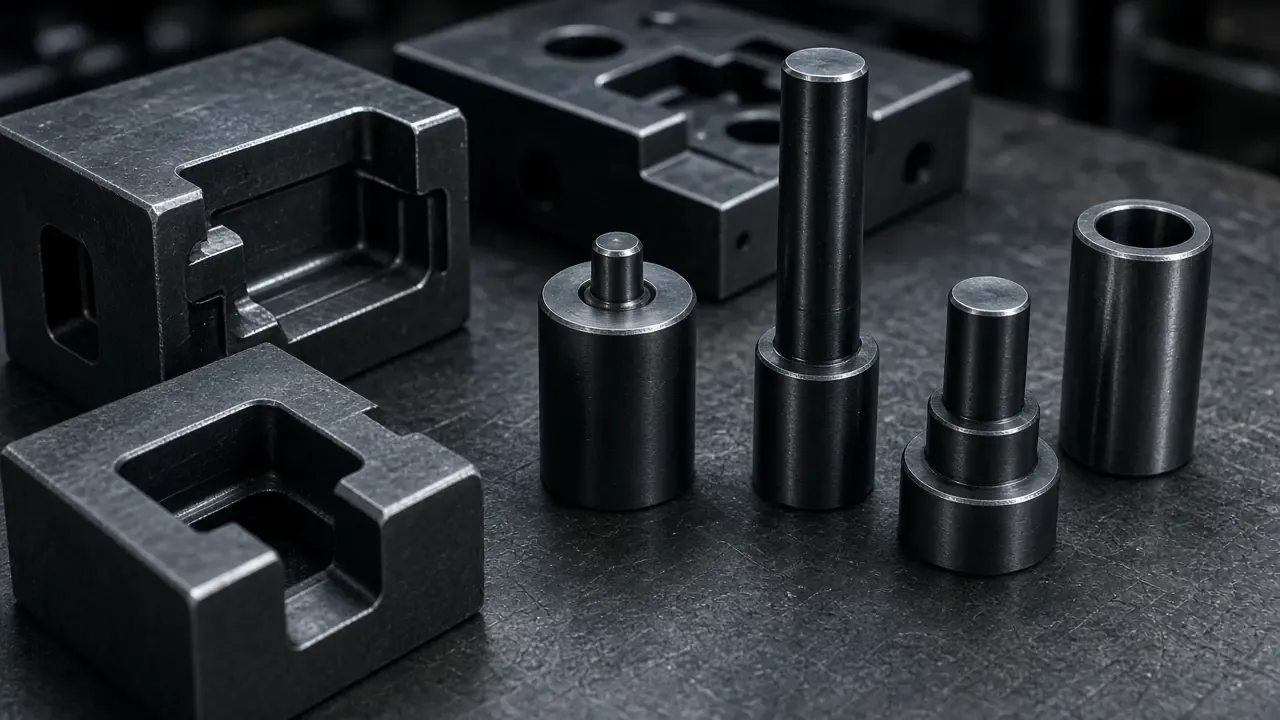
Ledeburitic high-alloy cold work tool steel with 12% chromium and about 1.55% carbon. Through-hardening, with high wear resistance and good dimensional stability.
01Material Properties
- High abrasive wear resistance
- Good adhesive wear resistance
- High compressive strength
- Adequate toughness
- Suitable for high-temperature tempering
- Suitable for coating after appropriate heat treatment
- Suitable for sub-zero treatment
- Good dimensional stability in heat treatment
02Applications
- Blanking, slitting and shearing dies and tools
- Tube and profile rolls and tooling
- Punches
- Drawing and forming dies
- Crushing balls and dies
- Industrial knives
- Hand knives
03Delivery Condition
- 255 HB, soft annealed
04Heat Treatment
Typical values
- Soft annealing
- 800–850 °C; max. 250 HB
- Stress relieving
- 600–650 °C
- Preheating
- Stepwise: 650 °C and 850 °C
- Hardening
- 1020–1050 °C; 15–30 min
- Quenching medium
- Air/pressurised gas, oil or 500–550 °C salt bath
- As-quenched hardness
- ≈ 63–65 HRC
- Tempering
- Low: 180–250 °C → 60–62 HRC; high (for PVD): 500–550 °C, 2–3 times → 58–60 HRC
- Working hardness
- 56–62 HRC
- Sub-zero
- Optional −70 °C (dimensional stability)
Heat treatment cycle (schematic)
Tempering diagram (approximate)
Values are approximate and for information only; they vary with section size, heat and furnace conditions. Binding values are determined from the manufacturer’s data under laboratory conditions.
Have a material requirement?
Send us your specification, drawing or RFQ. Our team will review the requirement and identify a suitable supply option.