O2 Cold Work Tool Steel
1.2842
- EN1.2842
- EN90MnCrV8
- AISIO2
Oil-hardening cold work tool steel with about 0.9% carbon, alloyed with manganese, chromium and vanadium. Good hardenability, low distortion in heat treatment and high dimensional stability.
01Applications
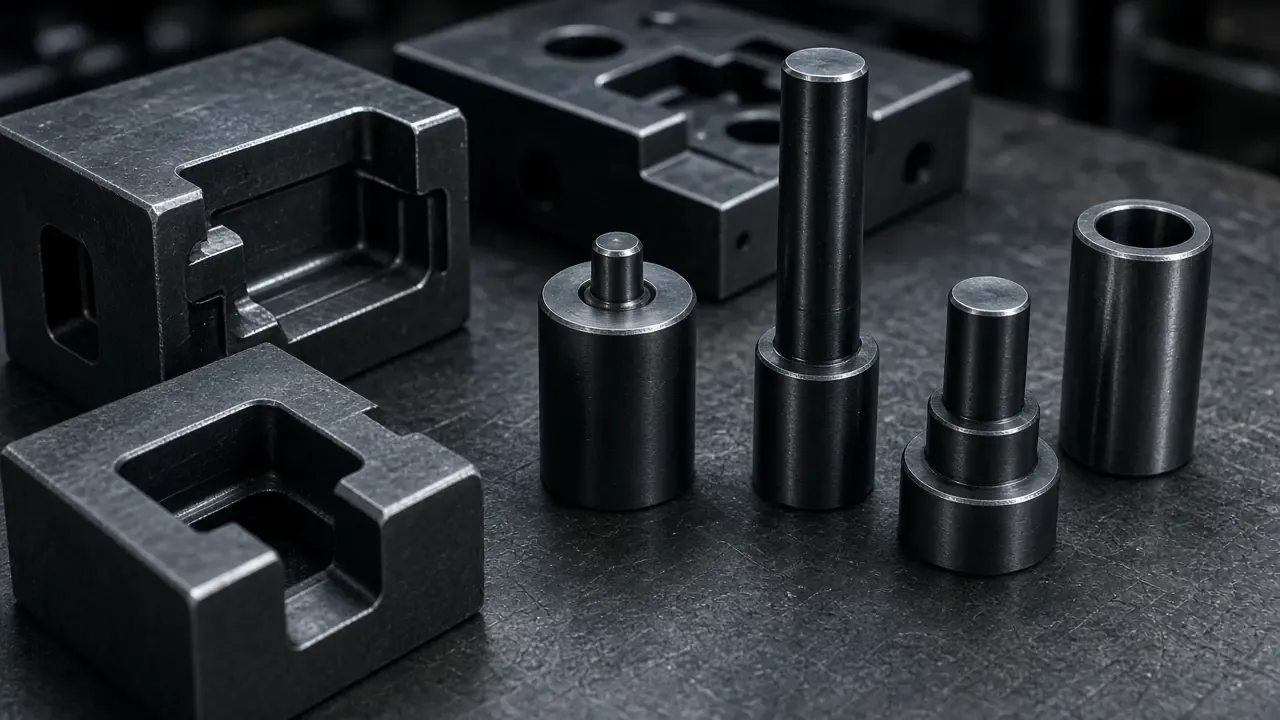
- Punches and small cutting knives
- Gauges and measuring tools
- Small blanking and bending dies
- Reamers and taps (low cutting speed)
02Heat Treatment
Typical values
- Soft annealing
- 680–720 °C; max. 229 HB
- Stress relieving
- 600–650 °C
- Preheating
- 600–650 °C
- Hardening
- 790–820 °C; 15–30 min
- Quenching medium
- Oil or 180–220 °C salt bath
- As-quenched hardness
- ≈ 63–65 HRC
- Tempering
- 150–300 °C, once or twice
- Working hardness
- 58–62 HRC
Heat treatment cycle (schematic)
Tempering diagram (approximate)
Values are approximate and for information only; they vary with section size, heat and furnace conditions. Binding values are determined from the manufacturer’s data under laboratory conditions.
Have a material requirement?
Send us your specification, drawing or RFQ. Our team will review the requirement and identify a suitable supply option.