O1 Tool Steel
1.2510
- EN1.2510
- EN100MnCrW4
- AISIO1
Oil-hardening general-purpose cold work tool steel with easy machining and low distortion. Widely used for small and medium-size cutting tools and gauges.
01Material Properties
- Oil hardening; low hardening temperature
- Easy machinability
- Good edge retention
- Low distortion
- Heat treated to 58–64 HRC
02Applications
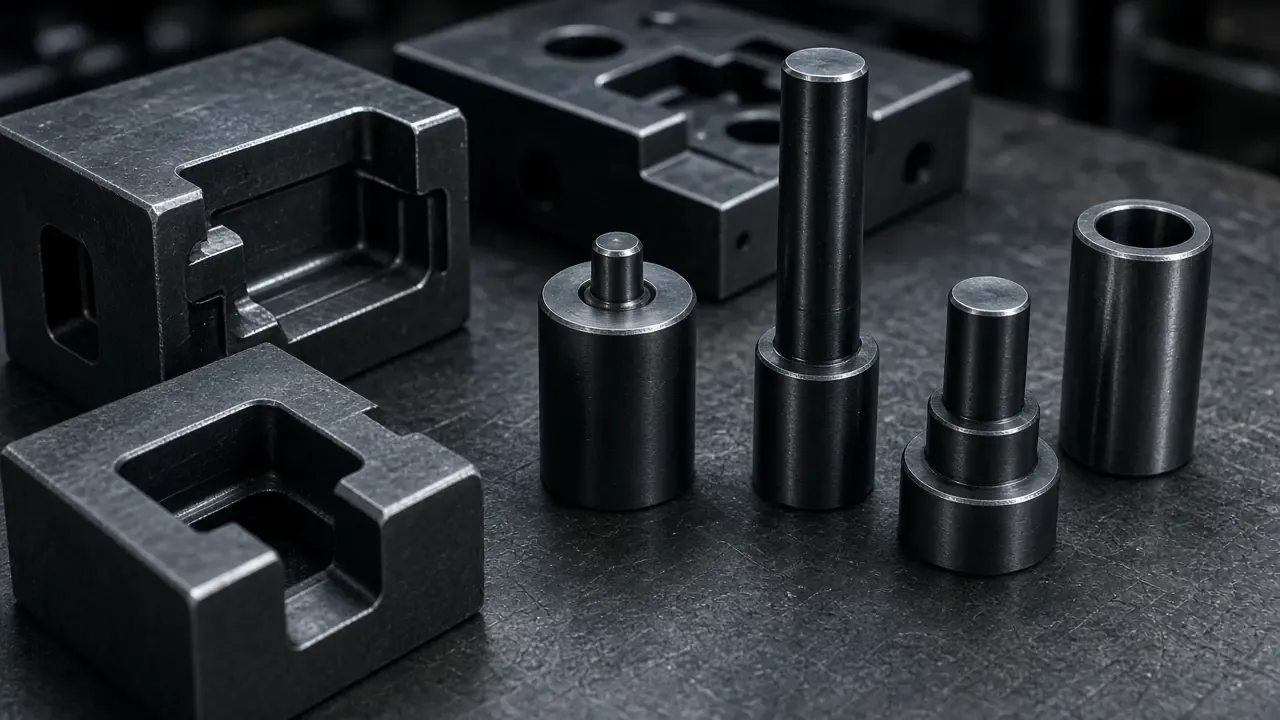
- Cutting and punching dies
- Reamers, taps and hand tools
- Woodworking knives
- Gauges and measuring instruments
- Small plastic molds and mold pins
03Delivery Condition
- Max. 229 HB, soft annealed.
04Heat Treatment
Typical values
- Soft annealing
- 710–750 °C; max. 229 HB
- Stress relieving
- 600–650 °C
- Preheating
- 600–650 °C
- Hardening
- 790–830 °C; 15–30 min
- Quenching medium
- Oil or 180–220 °C salt bath
- As-quenched hardness
- ≈ 63–65 HRC
- Tempering
- 150–300 °C, once or twice
- Working hardness
- 58–63 HRC
Heat treatment cycle (schematic)
Tempering diagram (approximate)
Values are approximate and for information only; they vary with section size, heat and furnace conditions. Binding values are determined from the manufacturer’s data under laboratory conditions.
Have a material requirement?
Send us your specification, drawing or RFQ. Our team will review the requirement and identify a suitable supply option.